Hey everyone, Sam here, and before we dive in—quick heads up: I’m not just some random blog guy. I’m the owner of a small, hardworking titanium bar supplier, so this isn’t just internet advice. This is stuff I’ve tested in my own shop, fixed when it went wrong, and refined over the last 8 years of dealing with everything from hobbyists’ tiny 1/4” bars to aerospace clients who’d ground me if I messed up their 6” billets. Titanium is my bread and butter, so when someone hits me up asking “how do I cut this without ruining it?” I don’t just send them a generic YouTube link. Let’s break this down. Titanium Bar
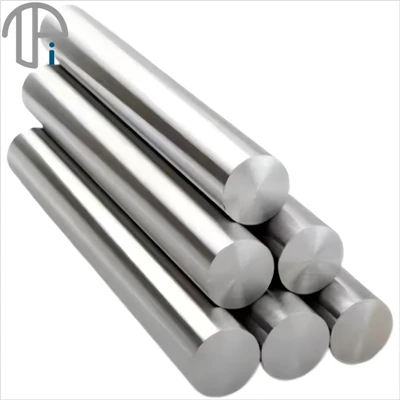
First off—wait, why even worry about cutting titanium? It’s not like cutting aluminum, that’s for sure. Titanium has this weird, counterintuitive superpower: it’s strong, but it’s also soft enough to gum if you rush it. And if you rush it, you get scrap bars, messed up blades, and even tiny shavings that can bite through gloves (trust me, I’ve been there—still have a scar on my index finger from a lazy cut on a 1” grade 5 bar). Most people think “just use a saw!” but titanium hates being pushed too hard, and it hates overheating more than anything. Overheat it, and it gets brittle—like, snap-in-half-while-you’re-trying-to-file-it brittle. Not good.
Let’s start with the basics: what kind of titanium bar are you cutting? That’s non-negotiable. I get calls every week from someone who bought a random cheap titanium bar from Amazon and is trying to cut it with a jigsaw blade. Don’t do that. Grades matter. Grade 2 (commercially pure, CP) is the softest—great for marine parts, stuff that needs to bend a little. Grade 5 (Ti-6Al-4V) is the workhorse, strongest, used for aerospace, bike parts, even medical implants. Grade 5 is way harder to cut than Grade 2, so you can’t use the same setup for both. Also, is it solid bar or a hollow tube? Wait, no, we’re talking bars here—so solid, round, flat, whatever, but the grade and diameter are make-or-break. If you’re cutting a 1/4” Grade 2 bar, that’s easy. Cutting a 6” Grade 5 billet? That’s a whole different job, needs different tools, different speed, different everything. I’ve seen a guy try to cut a 4” Grade 5 bar with a circular saw meant for wood—blunt the blade in 10 seconds. Waste of money, waste of time.
Next, tools. This is where I see most people mess up. Let’s go from small DIY stuff up to industrial, because not everyone’s got a shop full of CNC machines. If you’re a hobbyist cutting tiny bars (like 1/4” or smaller), don’t even think about a jigsaw. Jigsaw blades bounce, they overheat, they get clogged with titanium gunk. Your best bet here is a hacksaw with a bi-metal blade—18 to 24 TPI (teeth per inch). Higher TPI for thinner bars, lower for thicker? Wait, no—wait, 18 TPI works for most small titanium. Bi-metal is key because it’s made of high-speed steel (HSS) with a softer body, so it flexes a little instead of snapping. I keep a pack of these in my shop at all times—$5 a blade, way cheaper than buying a new circular saw. Also, for small stuff, a miter box to keep the cut straight is a must. I don’t care if you’re in a garage or a pro shop—straight cuts mean less filing later, and titanium filing is a pain.
If you’re upgrading to medium bars—like 1/2” to 2” Grade 5—you can step up to a bandsaw, but not just any bandsaw. You need a metal-cutting bandsaw, not one of those little ones for wood and plastic. Blade TPI here is 10 to 14. Lower TPI for thicker bars, higher for thinner. Also, bi-metal or carbide-tipped blades only. Carbide is more expensive, but it lasts way longer on titanium—worth every penny if you’re cutting more than a couple bars. Don’t use a wood bandsaw blade, I beg you. I once tested a wood blade on a 1.5” Grade 5 bar just to see what would happen—half the teeth snapped off, and I had to file the bar for an hour to get the cut even. Not worth it.
For anything bigger than 2”, industrial stuff, or if you’re cutting bars all day like my shop does? We use a circular saw with a carbide-tipped blade, or even a CNC lathe with a turning tool, but we’ll get to that later. The key tool here is coolant. You can’t skip coolant. Titanium generates a TON of friction when you cut it, and friction = heat = brittle titanium = scrap. If you’re using a hacksaw, you don’t need a fancy coolant, but a little WD-40 or cutting oil sprayed on the blade while you work works. I keep a spray bottle of soluble cutting fluid in my shop—mix it with water, way cheaper than straight oil, and it works just as good. For bandsaws, you hook up a dedicated coolant system to the blade, and for circular saws, you use a flood coolant that covers the whole blade and the bar. I’ve had clients send me bars they cut at home with no coolant—they came back with cracks and brittle edges, had to melt them down and re-machine them. Coolant isn’t a “nice to have” here, it’s non-negotiable.
Now, the actual cutting technique. This is where most people rush it, and that’s the #1 mistake. Let’s start with the pace. For small hacksaw cuts: slow, steady, even pressure. Don’t bear down like you’re trying to split a log. Take long strokes, let the blade do the work. I’ve seen people push so hard on a hacksaw blade that it snaps right in half, flying across the shop and almost hitting my intern (don’t tell the boss, but that intern’s still here, so it’s fine). For bandsaws: set the speed low. For Grade 5 titanium, that’s like 60 to 80 surface feet per minute (SFM). Way lower than you’d use for aluminum (which is like 300 SFM). If you run the bandsaw too fast, the blade will overheat, gum up, and dull in minutes. For circular saws, same thing—low speed, high torque. Don’t crank it up to max RPM, that’s how you burn the titanium.
Another big one: support the bar. Titanium is strong, but if you’re cutting a long bar (like 6 feet long) with only one end clamped, it will vibrate. Vibration = uneven cuts = rough edges = more work. I always clamp my bars in two places: one right next to the cut, and one a foot or so away, to keep it stable. For round bars, I use V-blocks to hold them—they stop the bar from rolling when you cut. I’ve had bars roll mid-cut before, and it’s not pretty. Blade goes off track, bar gets a nick, you’ve either got a scrap bar or a lot of sanding to do.
Wait, what about laser cutting or waterjet cutting? A lot of people ask about that for precision cuts. Those work, but they have their own rules. Laser cutting titanium can leave a heat-affected zone (HAZ) on the edge, which is that brittle stuff we talked about earlier. So if you’re using the cut bar for something critical—like a bike frame part or a medical implant—you have to grind off that HAZ after. Waterjet cutting is great, no HAZ at all, because it uses high-pressure water and garnet to cut, no heat. But it’s slower, and it’s not cheap if you’re cutting a lot of bars. My shop uses waterjet for small, high-precision custom parts, but for bulk bar cutting, we stick to bandsaws and circular saws—it’s faster and cheaper for our clients.
Now, post-cut stuff. Don’t just cut the bar and go have a beer. Titanium shavings are sharp, and the cut edge is rough, so you need to deburr it. A quick pass with a file, a wire brush, or even a sanding disc will get rid of the burrs. But wait—don’t use a metal file that’s already been used on steel. Steel shavings left on the file can contaminate the titanium edge, which is bad if you’re making parts for something like a boat or a bike (steel rust can eat into titanium over time). I have a dedicated set of tools just for titanium—file, wire brush, sandpaper—no mixing with steel stuff. Small detail, but it’s how you get parts that last.
Let’s talk about common mistakes I see all the time, so you don’t make them. First, using the wrong blade. Like I said, wood blades on metal cuts—game over. Second, rushing the cut. I had a client last month who cut a 2” Grade 5 bar in 2 minutes with a circular saw, no coolant. He sent it to us to machine for a custom bike part, and the edge was so brittle it cracked when we touched it with a lathe tool. We had to replace the bar, and he had to pay a rush fee for a new one. Don’t be that guy. Third, no coolant. Another client cut a dozen Grade 2 bars in his garage with only WD-40 sprayed on once. Half of them were bent from overheating, had to straighten them all before we could process them. Fourth, clamping wrong. I once had a bar slip in a vise because I didn’t pad the vise jaws. Titanium is soft, so it will get marked if you clamp it with bare steel jaws. I use rubber or copper jaws on my vise to prevent that—small thing, but it keeps the bar looking good and adds strength.
Wait, what about if you’re a total beginner with only a few bars to cut? Let’s say you bought a 1” Grade 2 bar for a DIY project. What’s your go-to setup? Grab a hacksaw with a bi-metal 18 TPI blade, get a small bottle of cutting oil, clamp the bar in a vise with soft jaws, take long, slow strokes, use oil on the blade every 10 or so strokes. If you mess up and the edge is rough, don’t panic—spend 5 minutes with a coarse sandpaper, then fine sandpaper, and you’re good to go. It’s not hard, you just have to take it slow.
Now, for the shop folks, cutting bulk bars: we have a dedicated bandsaw station just for titanium, we use carbide-tipped blades, run it at 70 SFM, flood coolant on the blade, and we always check the blade for gunk after every 5 bars. If the blade starts to look dull, we replace it before it starts burning the titanium. It might seem like a hassle, but it saves us a ton of money on scrap and replacement blades in the long run.
A quick safety note too—titanium shavings are flammable. If you’re cutting titanium with a bandsaw or a saw that produces fine shavings, don’t have any open flames around, and make sure your shop has a Class D fire extinguisher (for metal fires). Water works for small fires on steel, but it reacts with titanium and makes it worse. I learned that the hard way when a pile of shavings caught fire in my shop a few years back—grabbed a Class D extinguisher, put it out in 2 seconds, no damage. Worth the $100 for the extinguisher, trust me.
Wait, let’s circle back to why I know all this—because I’ve made every single mistake I just told you about. I started this supplier shop 8 years ago with nothing but a lathe, a used bandsaw, and a garage full of scrap titanium bars. The first order I ever got was for 10 1” Grade 5 bars for a local bike builder. I cut them with a wood blade, no coolant, rushed it, and half of them were bent and burned. I had to buy new bars, work for free to make up for it, and that bike builder still sends us all his parts today—nice guy, but he let me know I messed up, and I fixed it. That’s when I started testing everything, writing down what works, what doesn’t, so I don’t let anyone else make the same mistakes.
If you’re here because you need titanium bars to cut, or you already have some and are scared to ruin them—hit me up. I don’t do generic sales pitches. I can tell you which grade is right for your project, give you a free cutting guide specific to your bar size and type, no B.S. All I ask is that you tell me what you’re working on, so I can give you the best advice possible. No weird links, no bots, just me answering your questions straight.
Now, before I wrap this up, a quick recap to make sure you don’t forget anything:
- Know your grade: CP (Grade 2) is soft, Grade 5 is tough—adjust your tools/speed accordingly.
- Use the right blade: bi-metal for small cuts, carbide for medium/large, never wood blades.
- Coolant is non-negotiable: stop skipping it, it’s there to stop the heat that ruins titanium.
- Take it slow: rush cuts = scrap, period.
- Support and clamp properly: no rolling bars, no marked edges.
- Post-cut deburr, and keep your tools separate if working with steel.
That’s it. Titanium isn’t the scary metal everyone makes it out to be—you just have to work with it, not against it. I’ve cut bars for everything from custom jewelry to aerospace components, and once you get the hang of it, it’s way easier than you think. If you have any questions, or you need titanium bars for your next project, don’t hesitate to reach out. I’m here to help.
Titanium Nut References:
- ASM International. (2005). Titanium: Properties and Applications. Materials Park, OH: ASM International.
- Machining Data Handbook. (2020). 10th ed. Industrial Press, Inc.
- Titanium Suppliers Association. (2022). Best Practices for Cutting and Machining Titanium Bars. Technical Bulletin No. TB-007.
Baoji Top Titanium Industry Co., Ltd.
As one of the most professional titanium bar manufacturers and suppliers in China, we’re featured by quality products and good price. Please rest assured to buy bulk titanium bar in stock here and get quotation from our factory. Customized orders are welcome.
Address: No. 2, South Section Of Phoenix 2nd Road,High-Tech Zone, Baoji,Shaanxi, China (Mainland)
E-mail: sales@bjtopti.com
WebSite: https://www.china-topti.com/
